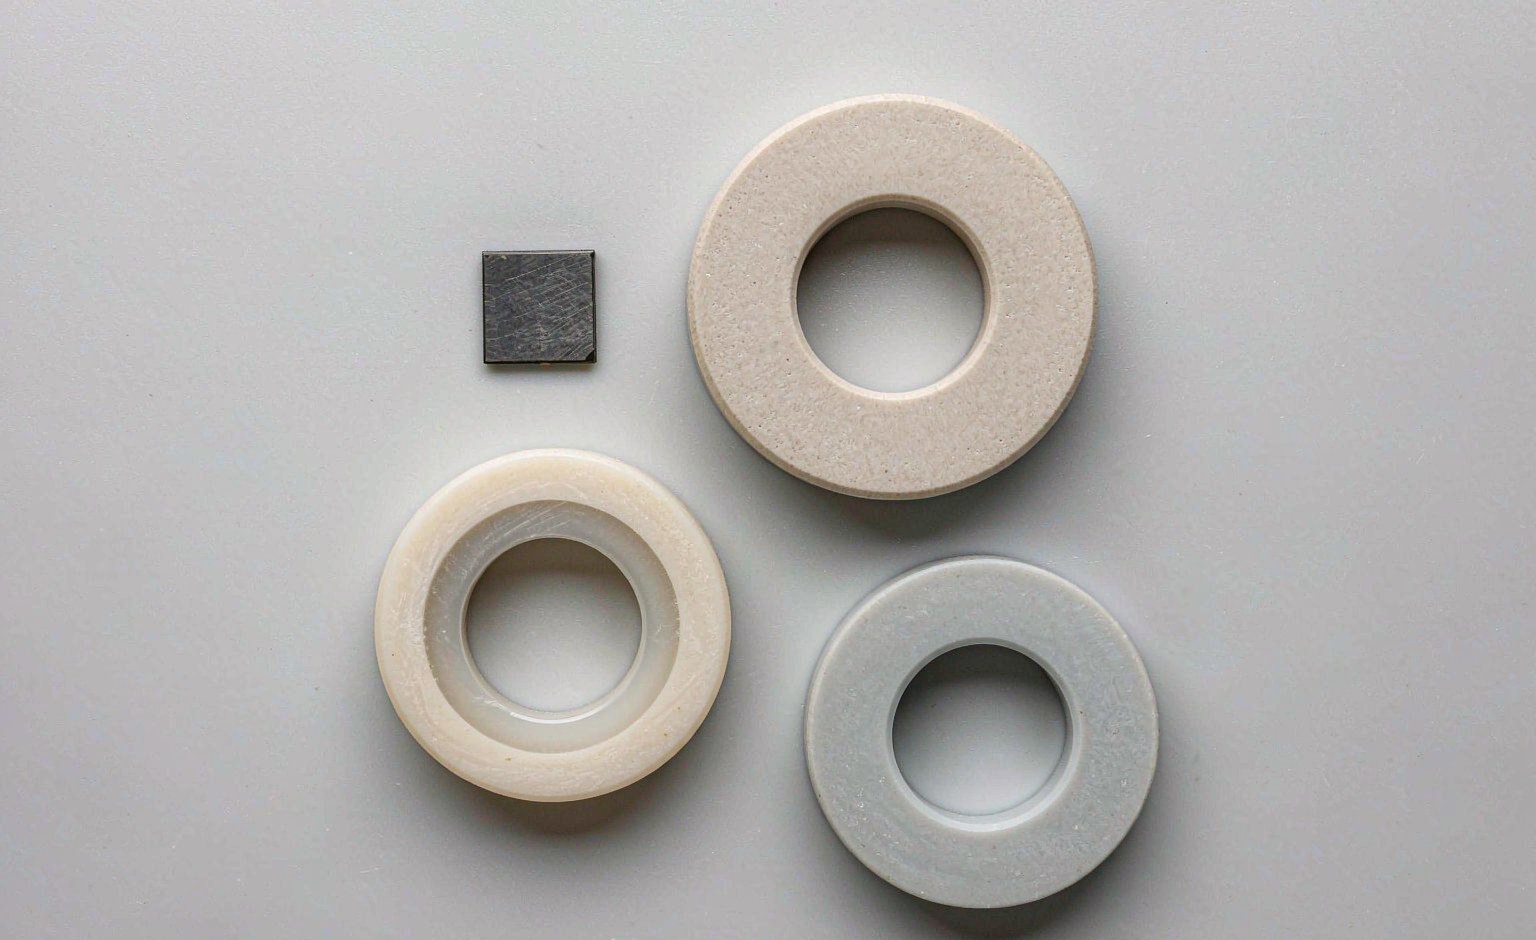
Technical ceramics are bought as blanks and sold as tolerances. Sintering a substrate and brazing copper onto it belong to the ceramics plants. Cutting it to a non-standard outline, grinding it to thickness, holding the warp, and proving it measured — that is the end of the chain where small batches stop.
A ceramics supplier that will not draw this line is telling you it does everything. Nobody does everything.
The mistake in this category is picking the material with the best single number. Every grade here wins one column and loses another.
| Material | What we machine | Why it gets picked | What it gives up |
|---|---|---|---|
| Alumina Al₂O₃ 96% / 99.5% |
Discs, rings, washers, standoffs, insulators, wear plates | Cheapest per part, good dielectric strength, available in every thickness | 20–30 W/(m·K) and fracture toughness around 3.5–4.0 MPa·m1/2 — it cracks under fast thermal cycling |
| Zirconia 3Y-TZP |
Plungers, sleeves, blades, wear faces, small precision parts | Highest strength and toughness of the common grades; takes a fine surface finish | Low thermal conductivity, and it degrades in hot steam — not a furnace material |
| Silicon nitride Si₃N₄ |
Substrate blanks, plates, rollers, guide parts, wear rings | Toughness 6–8 MPa·m1/2 with 600–900 MPa bending strength — survives thermal shock that destroys alumina | Grinding is slow and diamond-bound; the material is expensive per blank |
| Aluminium nitride AlN |
Heat-spreader plates, insulating washers, thin discs | 170–220 W/(m·K) — the highest conductivity of the electrically insulating ceramics | Brittle: toughness only 2.5–3.5 MPa·m1/2. It is a heat path, not a structural part |
| Silicon carbide SSiC / RBSiC |
Seal rings, nozzles, liners, pump parts | Hardness and wear resistance at temperature; chemically stable | Not an electrical insulator in the grades we machine — do not specify it for isolation |
| Machinable glass-ceramic Macor-type |
Prototype fixtures, feedthrough bodies, lab parts, single pieces | Cut and drilled with ordinary carbide tooling — no diamond, no green machining | Modest strength; a prototyping material, not a production one |
A sintered blank is not a part. It becomes one in this order — and the step that usually goes wrong is not the one people watch.
Thickness, parallelism and flatness. A sintered substrate arrives with roughly 20% shrinkage already baked in, so the blank is near-size and the grinder only removes the difference. This is the slow, expensive, diamond-bound stage.
Surface finish for bonding or for sealing faces. Ra target comes from your drawing: Ra RANGE WE HOLD.
Non-standard outlines, windows and slots. Thin substrate is where chipping starts, so the cut sequence matters more than the cut speed. CUT METHOD AND KERF WIDTH
Grinding media and diamond residue have to come off before inspection, or every measurement is measuring the dirt. Note for fluoride users: silicon nitride is attacked by hydrofluoric acid — it is the one chemical this material does not tolerate.
Controlled, because a wet porous ceramic measures wrong and packs worse.
Thickness, TTV, warp and dimensions are measured here and reported. Bond-layer inspection by scanning acoustic microscopy is outsourced — we do not own a SAM and we will not pretend a visual check replaces one.
Edge-protected, plate-separated, because a chipped corner is a scrapped part and freight is not gentle.
The step that decides the batch is step 01 and step 02 — not the cutting everyone photographs. Grinding and polishing parameters drift, and a drift shows up as a warp or a thickness spread across the lot, not as one bad part you can see. Which is why the useful question to ask any supplier in this category is not "what machine do you have" but "how do you know the lot is consistent".
Small batches, one drawing at a time. The volume end of this industry does its post-processing in-house, and we are not built to compete with it.
One piece, one drawing, one deadline. Test rigs, insulating parts, sample holders, Macor-type prototypes before anyone commits to a mold. This is the batch no ceramics plant wants and no ordinary machine shop can hold.
Replacement plates, feedthrough bodies, chamber furniture and fixtures. Low volume, high mix, and a machine that is down until the part arrives — so the drawing matters more than the price.
A ceramic part that works in a demo and now has to work in 200 units. Too small for a ceramics plant to schedule, precise enough that a general machine shop will scrap it.
A worn nozzle, a cracked guide, a seal ring with a supplier that no longer exists. Measure the original, model it, remake it in the right grade.
One is about choosing the grade. One is about holding the tolerance.
SN60 to SN120, why conductivity and strength pull against each other, the thickness trick that lets silicon nitride match aluminium nitride, and the eight boundaries nobody puts in a brochure.
What is done here, what is sent out, what gets measured, how consistency is proven across a lot, and the five questions buyers ask before they send a blank.
It is not a claim to be a ceramics manufacturer. If your program needs a sintered substrate with copper already bonded, you need an AMB house, and we will say so in the first reply rather than quote around it.
What it is: a shop that takes the blank the ceramics plant made and turns it into the part your drawing describes, with the measurement to prove it. For a program between prototype and production, that is usually the piece that is missing.
Material grade, blank size, finished thickness, tolerance and quantity. If the blank already exists, tell us who made it — it changes which grinding sequence we use.
Get a quote